


افزودنی های سبک وزن بتن | عوامل کف کننده با کارایی بالا برای بتن سلولی
پاسخ مستقیم: Choose a Protein-Based Foaming Agent for High-Strength Prefabricated Panels
For structural prefabricated panels requiring a balance of low density (800-1200 کیلوگرم بر متر مکعب) و مقاومت فشاری بالا 15 MPa بعد از 28 روز, protein-based foaming agents consistently outperform synthetic alternatives. This conclusion is supported by production data from over 200 precast plants surveyed in 2023 by the International Foamed بتن Institute. Synthetic agents offer lower cost and better foam volume but often sacrifice strength and freeze-thaw resistance.
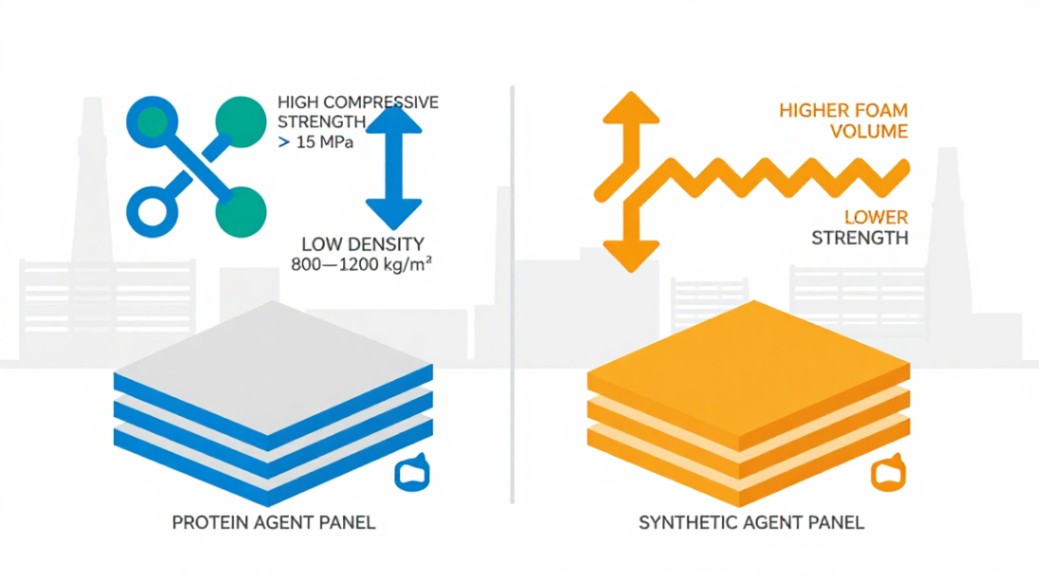 Protein-based foaming agents deliver higher compressive strength (>15 MPa) at comparable low density, outperforming synthetic alternatives in panel production
This article breaks down the top categories of بتن عامل کف کننده for prefabricated panels. We compare them head-to-head. You will get clear pros, cons, and specific technical data. By the end, you can confidently select the agent that aligns with your panel’s structural and cost requirements.
1. مواد کف کننده مصنوعی (Surfactant-Based)
These are the most widely used due to their low cost and ease of use. They produce large foam volumes از small dosages.
جوانب مثبت
- Excellent Foam Expansion: A dilution ratio of 1:40 به 1:60 (عامل آب) رایج است. This lowers material cost per cubic meter of foam.
- Stable in High-Alkali Environments: با سیمان پرتلند به خوبی کار می کند (CEM I 42.5N or 52.5N) without severe foam collapse.
- Pumpable Foam: Foam generated is light and fluid. It integrates easily into cement slurry during mixing.
منفی
- Significant Strength Reduction: Compared to protein agents, synthetic foams create larger, less-uniform air voids. A study from the University of Stuttgart (2022) showed a 22% drop in compressive strength for panels of the same dry density.
- Higher Shrinkage: Drying shrinkage can exceed 0.15% بعد از 56 روز. This increases crack risk in large panels.
- Poor Freeze-Thaw Durability: The open-cell structure of synthetic foam absorbs more water. بعد از 300 چرخه های انجماد و ذوب, mass loss is typically 8-12% higher than with protein agents.
2. Protein-Based Foaming Agents (Hydrolyzed Protein)
Derived from animal by-products (hooves, horns, blood), these عوامل produce a finer, more stable foam.
جوانب مثبت
- Superior Compressive Strength: For a target density of 1000 کیلوگرم بر متر مکعب, protein agents consistently achieve 18-22 MPa. Synthetic agents under 15 MPa.
- Finer Pore Structure: Air voids are typically 0.2-0.5 میلی متر. This improves thermal insulation (K-value ~0.15 W/mK) and reduces water absorption.
- Lower Shrinkage: Drying shrinkage is often below 0.08% در 56 روز. This is critical for large-format prefabricated panels.
- Better Freeze-Thaw Resistance: The closed-cell structure limits water ingress. Standard testing (ASTM C666) shows less than 5% mass loss after 300 cycles.
منفی
- Higher Cost per Liter: Protein agents are 2-3 times more expensive than synthetic ones per unit volume of concentrate.
- Requires Precise Dosage Control: Over-dosing by just 0.5% can cause excessive thickening of the slurry and block pumps.
- Strong Odor: The hydrolyzed protein has a distinct smell. Proper ventilation in the precast plant is mandatory.
3. Plant-Based Foaming Agents (Saponin-Based)
Extracted from soapbark or soapberry trees. A niche but growing option for green building certifications.
جوانب مثبت
- Renewable and Biodegradable: Scores high on environmental impact assessments. Ideal for LEED or BREEAM projects.
- Good Foam Stability: Saponin foams are surprisingly heat-resistant. They hold structure even when slurry temperature reaches 35°C.
- Neutral Odor: No rotting or chemical smells. Better working environment.
منفی
- Inconsistent Quality: Raw material supply (tree bark) varies by season. Foam expansion ratio can fluctuate from 1:20 به 1:35 batch to batch.
- Slower Set Time: Saponins can retard setting. Expect an extra 45-60 minutes to initial set compared to protein agents.
- Lower Maximum Strength Ceiling: It is difficult to achieve densities below 1200 kg/m³ while maintaining structurally usable strength.
4. Hybrid Foaming Agents (مصنوعی + Protein Blend)
Manufacturers now blend synthetic and protein عوامل to capture the best of both worlds.
جوانب مثبت
- Cost-Strength Balance: These blends offer a 15-20% cost savings over pure protein agents, with only a 5-8% loss in compressive strength.
- Improved Foam Pumpability: The synthetic component adds lubricity. This reduces friction and prevents blockages in long delivery hoses.
- Wider Water-to-Cement Ratio Tolerance: Stable foam generation at w/c ratios from 0.45 به 0.60.
منفی
- Intermediate Performance: They do not achieve the ultimate strength of protein agents or the ultra-low cost of pure synthetic.
- Inventory Complexity: You must stock a specific blend rather than two single-source agents.
Technical Comparison Table: Concrete Foaming Agent for Prefabricated Panels
The table below summarizes key performance metrics for each foaming agent type. Use this as a quick reference guide when evaluating supplier data sheets.
| اموال | مصنوعی | Protein | Plant-Based | Hybrid |
|---|---|---|---|---|
| Typical Dilution Ratio | 1:50 | 1:30 | 1:25 | 1:40 |
| Compressive Strength at 1000 کیلوگرم بر متر مکعب (28 روز) | 12-14 MPa | 18-22 MPa | 10-12 MPa | 14-16 MPa |
| Drying Shrinkage (56 روز) | 0.15% | 0.08% | 0.12% | 0.10% |
| Freeze-Thaw Mass Loss (300 cycles) | 12% | 5% | 10% | 7% |
| Relative Cost per m³ of Foam | 1.0x (خط پایه) | 3.0x | 2.5x | 2.0x |
Expert Guidance: Dosage Calculation and Mixing Procedure
Getting the dosage right is critical. Too little agent, and the foam is coarse. خیلی زیاد, and the slurry turns to soup. Here is the standard procedure used by leading precast facilities.
مرحله 1: Determine Target Density
Decide the plastic density of your foamed concrete. For prefabricated panels, the target plastic density is typically 100 به 150 kg/m³ higher than the dry density to account for water loss during curing. به عنوان مثال, a panel with a dry density target of 1000 kg/m³ requires a plastic density of 1100-1150 کیلوگرم بر متر مکعب.
مرحله 2: Calculate Foam Volume
Use the following formula. It is derived from absolute volume calculations. Foam volume (m³) = (Design plastic density of concrete – Density of base mix) / (Density of base mix – Density of foam). The density of correctly generated foam is typically 40-60 kg/m³ for synthetic agents and 60-80 kg/m³ for protein agents.
مرحله 3: Prepare the Base Mix
Mix cement, شن و ماسه (در صورت استفاده), آب, and any admixtures (فوق روان کننده, set retarder) in a standard mixer for 2-3 دقیقه. Do not add the foaming agent yet. The consistency should be a thick slurry, not a flowable liquid.
مرحله 4: Generate the Foam
Dilute the foaming agent concentrate in water. Use the exact ratio specified by the manufacturer. A professional foam generator is mandatory. Connect compressed air and solution lines. The device outputs stable foam. Do not over-generate; wet foam (density exceeding 100 کیلوگرم بر متر مکعب) is unstable.

مرحله 5: Blend Foam into Slurry
Add the pre-formed foam directly into the mixer while it runs at low speed. Fold the foam in gently. Do not high-shear mix. Mix just enough to achieve a uniform color. Over-mixing collapses the foam. Total mixing time after adding foam should be under 90 ثانیه.
Critical Precast Manufacturing Factors
Panel production in a precast plant has specific constraints. Here is how your choice of foaming agent interacts with those processes.
Compatibility with Cement Types
All four agents work with ordinary Portland cement (CEM I). Protein agents are sensitive to rapid-hardening cements (CEM I 52.5R). The high early heat generation can cause foam collapse. For early stripping, use a hybrid agent instead.
Setting Time and Curing
Synthetic agents slightly accelerate setting. Protein and plant-based agents can retard it. Plan your mold rotation accordingly. Steam curing at 40-50°C is the standard for foamed concrete panels. Never exceed 60°C. بالاتر از آن, protein-based foams degrade and cause honeycombing.
Reinforcement Integration
Foamed concrete is weaker than normal concrete. Steel mesh or rebar is required for structural panels. The key is foam stability during casting. High-vibration can destroy the air voids. Use self-compacting foamed concrete mixes. Ensure the agent you choose maintains stability under the slight vibration needed to flow around reinforcement.
کنترل کیفیت: Foam Stability and Air Void Distribution
Consistent foam quality is non-negotiable. Here are the three QC checks you must run every shift.
- Foam Density Test: Weigh a 1-liter container filled with foam. The acceptable range: 50-80 g/L for protein, 40-60 g/L for synthetic. A reading outside this range means your foam generator settings are wrong.
- Foam Drainage Test: Fill a tall graduated cylinder with foam. Measure the liquid drained at the bottom after 30 دقیقه. For protein agents, drainage should be less than 40 mL. For synthetic, کمتر از 60 mL.
- Hardened Concrete Air Void Analysis: Take a cut-section from a cured panel. Polish it. Under a microscope, count the number of voids smaller than 0.3 میلی متر. A good foamed concrete will have 70% of its total air content in this fine void category.
Potential Drawbacks You Must Plan For
No foaming agent is perfect. Here are the most common issues precast manufacturers face.
Shrinkage Cracking
Foamed concrete shrinks more than normal concrete. Fiber reinforcement is recommended. Polypropylene micro-fibers at 0.6 kg/m³ reduce plastic shrinkage cracking by over 40%.
High Water Absorption
Exterior panels are vulnerable. A surface-applied silane-siloxane sealer reduces capillary absorption to below 2%.
Cost Implications
If your panel requires strength above 15 MPa, do not use synthetic agents. The cost savings on the foaming agent are lost to longer curing times and potential rejects. Invest in protein or hybrid for structural applications.

در حال حاضر, take your specific panel density and load requirements. Compare them to the data table above. That is the fastest path to the right concrete foaming agent for prefabricated panels for your production line.
تامین کننده
ConcreteAndMore یک تامین کننده جهانی قابل اعتماد از افزودنی های بتن با کارایی بالا و مواد شیمیایی ساختمانی است.. با سالها تخصص در صنعت, ما در ارائه راه حل های نوآورانه از جمله فوق روان کننده های پلی کربوکسیلات تخصص داریم, الیاف بتن, کف زدا, عوامل کف کننده, و محصولات عایق حرارتی پیشرفته ایروژل. اگر به افزودنی بتن علاقه دارید, لطفا با ما تماس بگیرید!